


Armory Sponsor


Posted: 5/29/2025 7:56:16 PM EDT
|
I'm planning a a couple cans. one for .30cal including .308 and down, the other deidicated 5.56. I'm going with a welded/tubless design for both. Both sets of baffles will be 60* cones. All parts will be 17-4ss H900. My question is what thickness should the skirts be? |
|
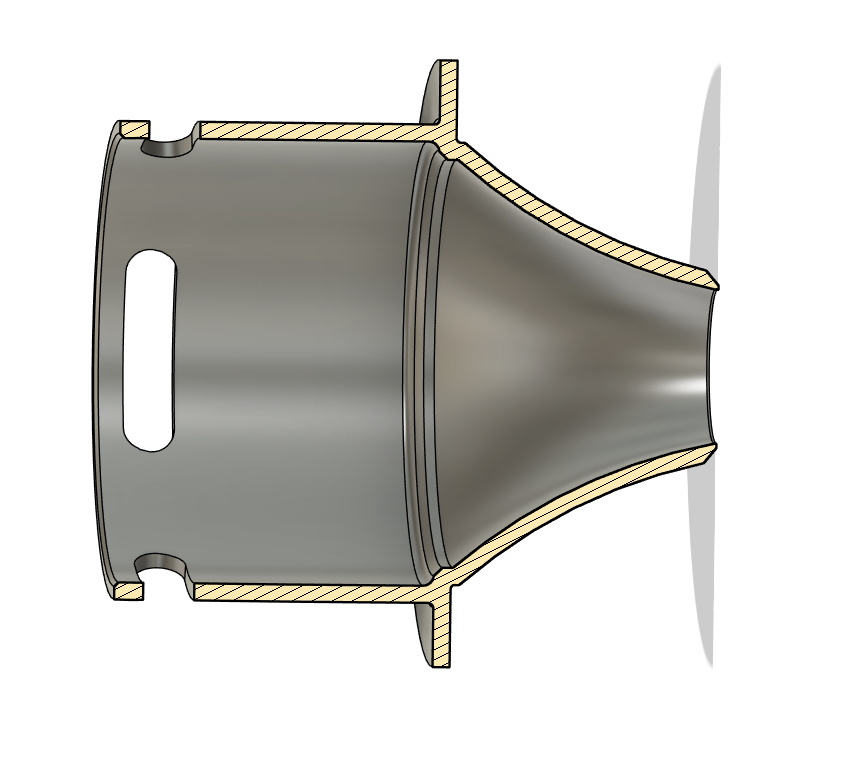
I designed some conically shaped baffles from 17-4 designed to be autogenously welded (fusion weld, no filler, back purged,on a turn table) into a baffle stack at around .040". This is a bolt action 300 blackout subsonic only. I would say .060" thickness would be sufficient for super sonic. https://tinypic.host/image/image.Dwe4w |
Joined:
Jun 2022
Posts:
48
EE: 0% (0)
 OR, USA

Husher of boomsticks
Joined:
May 2023
Posts:
682
EE: 0% (0)
CO, USA
|
The blast chambers on our Accipiter and Valkyrie models are .06" thick, the baffle walls get progressively thinner toward the distal end from .055" down to as thin as .035" on the longer ones. Of note, however, is that they are machined with a reinforcing ring in the blast chamber, blast baffles are threaded and welded into the blast chamber, and the baffle skirts are undercut to those thicknesses with all abutment faces .080". As mentioned, you would want to heat treat again post-weldment to retemper the material in the HAZ. |
Suppress all the things!
|
Originally Posted By ECCO_Machine: The blast chambers on our Accipiter and Valkyrie models are .06" thick, the baffle walls get progressively thinner toward the distal end from .055" down to as thin as .035" on the longer ones. Of note, however, is that they are machined with a reinforcing ring in the blast chamber, blast baffles are threaded and welded into the blast chamber, and the baffle skirts are undercut to those thicknesses with all abutment faces .080". As mentioned, you would want to heat treat again post-weldment to retemper the material in the HAZ. Are you saying heat treat the baffles such as to H900, then weld, and then re-treat to h900 to bring the weld HAZ up to strength? Or do I have that wrong? |
Armory Sponsor