


Posted: 8/15/2025 5:31:20 PM EDT
[Last Edit: Amish_Bill][Edited]
|
.. well, does it actually count as "chips" if I was reshaping some plastic to make an antenna fit? It turns out semi-rubbery plastic is a real pain to trim. At least I had two so I could learn something in the process. Attached File Attached File |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman

|
Thanks for the info. I went the other way - 220rpm and left the cutter that was mounted when I bought it. I figured that if something was going to go weird trying to trim plastic, 220 was going to be almost 4 times less bad than 800.  Feed was nice and slow by hand. I can also say that getting one with a DRO on it was a Smart Move (TM). I started many decades too late to rely on MK1 Eyeball for anything precise. |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
|
The trick with soft stuff is that you want it to cut clean with no load. If you force it (dull cutter), it will grab the part and cause it to rapidly leave the area. Just wait till you learn the DRO shortcuts/hacks. You can either use it to track actual dimensions, or to track cuts. Then some have whole tool libraries so you can swap cutters and retain accurate positioning. |
|
Originally Posted By Boostinjdm: ... Just wait till you learn the DRO shortcuts/hacks. You can either use it to track actual dimensions, or to track cuts. Then some have whole tool libraries so you can swap cutters and retain accurate positioning.  Attached File |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman

|
...and now it's First Chips on the Mill too. The original owner got the wrong size fixture set for this table. A few of the T-nuts were reduced to the right size, but not all. Earlier tonight there were three that still needed to be modified. Now there are two. I hear using your tools to make/fix more tools is the gateway drug in metalwork, eh? Attached File |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman

|
Originally Posted By Boostinjdm: Probably the wrong insert for the job. For plastic and soft things, HSS ground to a point and honed razor sharp works well. High rpm and slow feed also. Yep, the softer the material is the sharper your tools need to be. I've ground off the honed edge on carbide inserts to get a good sharp edge, just remember to not use it on steel as it will not last very long. |
Life's battles don't always go to the stronger or faster man. In the end, the one who wins is the one who thinks he can! - SCI, NRA
Team Ranstad
Team Ranstad
|
If I have to do those soft adapters again, I have some fresh parting tools I can grind on. I should be able to get a sharp hook on an end. The next task I have in mind is a small spacer turned on the lathe. PSA's JAKL has a weird diameter barrel that doesn't work well with timing shims. I can only think of a few ways that could go sideways.  |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman

|
Originally Posted By Boostinjdm: Probably the wrong insert for the job. For plastic and soft things, HSS ground to a point and honed razor sharp works well. High rpm and slow feed also. OP, if you don't want to mess with grinding HSS tools, you can buy HSS inserts. They're great for aluminum and other soft materials. 
|
EP429: Today's lesson - Don't provoke ARFCOM. People will see your butthole.
|
Finally - REAL chips being made ... It didn't take me long to figure out the steering on a forklift or backing a trailer, but this unholy three-way of handwheel motion, bed movement and bit movement relative to the part is wearing me out. I've only gone down 0.30" and I've already made at least 3 hard to miss mistakes. I had originally intended to leave this as a manual for a while. Learning to not fuck up in manual has me wanting to install the CNC parts.  Oh darn - I may have to turn this one into a skeletonized monstrosity to hide the evidence. Attached File |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
|
Originally Posted By Boostinjdm: Probably the wrong insert for the job. For plastic and soft things, HSS ground to a point and honed razor sharp works well. High rpm and slow feed also. Originally Posted By Boostinjdm: Probably the wrong insert for the job. For plastic and soft things, HSS ground to a point and honed razor sharp works well. High rpm and slow feed also. This. I also had specific cemented carbide tools ground the same way for Delrin and Nylon. We used to make urethane cup seals from 90A rod stock. Originally Posted By SandHillsHillbilly: Next time throw it in the freezer overnight before machining. I tried this and dry ice. It might work on a a single part with a quick cut, but it heats back up fast and and dimensions are all over. |

|
If I recall properly, you have to find one of the links with a file type extension to embed it here. You may see the image because it's cached in your browser.
|
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman

|
OP..... Pony up the money and install the I-gauging DRO conversion kit for the X, Y, and Z It will make your mill operations WAAAAAY easier. It may require some drilling/tapping to mount the brackets that hold the reader, and maybe fabricate a custom bracket or 2, but well worth the effort. You'll also need to make a flat steel panel, and then mount it to the left side of the head for the readouts. Be sure to label the read outs. When you look at the bottom pics of my mill, you'll see the sensor beams mounted. You'll also see the plate I made to mount the DRO read outs that use magnets to attach them.  Attached File Attached File Attached File |
Occid Vel Occisus Est !!

|
Originally Posted By Amish_Bill: I hear using your tools to make/fix more tools is the gateway drug in metalwork, eh? https://www.ar15.com/media/mediaFiles/1410/Mill_First_Chips_-800_jpg-3608974.JPG Yep, welcome to the rabbit hole |
|
Originally Posted By IdahoPCCinc: OP..... Pony up the money and install the I-gauging DRO conversion kit for the X, Y, and Z It will make your mill operations WAAAAAY easier. It may require some drilling/tapping to mount the brackets that hold the reader, and maybe fabricate a custom bracket or 2, but well worth the effort. You'll also need to make a flat steel panel, and then mount it to the left side of the head for the readouts. Be sure to label the read outs. ... Can't deny... I would like a DRO on the mill - the DRO on my lathe lets me know just how much nicer it would be. Is your IGaging reference just what you have, or is it known to be better than other chinesium? It looks like your 3 axis kit will be under $200. I'm also seeing single head 3 axis sets from others starting about $100 more. It would be an easier decision if I didn't have the ballscrews w/ mounts, Acorn box and steppers in the next room. (heck of a deal when I got the mill) I'm at the point where I don't have enough experience to know if I want to go manual w/DRO or CNC w/Acorn. I'm leaning towards CNC, but I also want to learn a bit by hand before I commit. SOooooo back to mangling an innocent 80 by hand. : - ) |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
|
Originally Posted By Amish_Bill: Can't deny... I would like a DRO on the mill - the DRO on my lathe lets me know just how much nicer it would be. Is your IGaging reference just what you have, or is it known to be better than other chinesium? It looks like your 3 axis kit will be under $200. I'm also seeing single head 3 axis sets from others starting about $100 more. It would be an easier decision if I didn't have the ballscrews w/ mounts, Acorn box and steppers in the next room. (heck of a deal when I got the mill) I'm at the point where I don't have enough experience to know if I want to go manual w/DRO or CNC w/Acorn. I'm leaning towards CNC, but I also want to learn a bit by hand before I commit. SOooooo back to mangling an innocent 80 by hand. : - ) Those pics are of my current set-up. The I-Gauging set-up is a good value for what it is. Amazon has the 3 axis kit for $185. The only issues I had with it was forgetting to turn off the display-which kills the battery in a week. And when I was 1st milling aluminum lowers using a water-based coolant spray. If the spray was too much, or aimed poorly, it would get on the sensor bar and cause erroneous readings. So....just remember to turn off the displays, keep the coolant off the sensor bars, and they work great. I-Gauging 3 piece kit on Amazon link. What I did for lowers was to write a step by step procedure, and printed it out. Stick it on a clip board, and read off of it while doing the work. Find the edge... do the math to find center line, then zero the Y Find the end to start from (usually .120 from the bolt catch) and start my path going back and forth watching the displays and matching the numbers on my procedure. Then it was just a matter of milling the center line, going + and minus on the Y axis, milling the edges of the trigger pocket, and then the rear pocket portion. After it was all roughed out, do a final pass of .010 to leave a nice finish, and to get the dimensions within +/- .002 of the print. You'll also have to figure out your speeds, feeds, and end mill cutter selection. Learn the difference between climb cutting vs conventional cutting. This is important when milling a pocket. And using an edge finder and doing the math to get into the center accurately is another skill to practice. Knowing exactly where you are is critical for milling accurately.  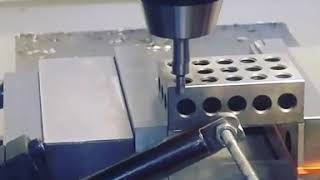 How to use an edge finder(2) |
Occid Vel Occisus Est !!

|
Originally Posted By IdahoPCCinc: Those pics are of my current set-up. The I-Gauging set-up is a good value for what it is. Amazon has the 3 axis kit for $185. The only issues I had with it was forgetting to turn off the display-which kills the battery in a week. And when I was 1st milling aluminum lowers using a water-based coolant spray. If the spray was too much, or aimed poorly, it would get on the sensor bar and cause erroneous readings. So....just remember to turn off the displays, keep the coolant off the sensor bars, and they work great. I-Gauging 3 piece kit on Amazon link. What I did for lowers was to write a step by step procedure, and printed it out. Stick it on a clip board, and read off of it while doing the work. Find the edge... do the math to find center line, then zero the Y Find the end to start from (usually .120 from the bolt catch) and start my path going back and forth watching the displays and matching the numbers on my procedure. Then it was just a matter of milling the center line, going + and minus on the Y axis, milling the edges of the trigger pocket, and then the rear pocket portion. After it was all roughed out, do a final pass of .010 to leave a nice finish, and to get the dimensions within +/- .002 of the print. You'll also have to figure out your speeds, feeds, and end mill cutter selection. Learn the difference between climb cutting vs conventional cutting. This is important when milling a pocket. And using an edge finder and doing the math to get into the center accurately is another skill to practice. Knowing exactly where you are is critical for milling accurately. https://m.media-amazon.com/images/I/419NE9B2SjL._SL1154_.jpg  https://www.youtube.com/watch?v=xTmmeP01zJs Sound advice. Im 10ish years into igaging dros on my mini mill. No regrets at all. I did opt for the tablet dispaly and touchdro. |
A firearm is like a parachute, if you need one but don't have one, you'll probably never need one again. IG @jimstagramguns

|
The 0.500 4 flute was just what I had in the mill, and I decided to just run with it. I have a smaller 3 flute to try next. I don't think I have any 2 flute though. I'll put one to play with on my wishlist for the next time I have spending money. |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
|
Originally Posted By OneMoreAR: I always used a 2-flute endmill in aluminum. They can make big chips in the soft metal and allow clearance for those chips. 2 or 3 flute is GTG. A few things to remember with using either is correct rpm's for cutter diameter, width/depth of cut (face and Z) and direction of cut. Always be aware of how much stick out you have with your tooling. All this can be found with a little internet digging or getting a copy of the machinist's hand book, (look for a cheap used one) and it does help when it comes to preventing chatter, tool life, breaking shit, etc. Lubricant type can help with finish and cut quality too. . |
Occid Vel Occisus Est !!
|
Originally Posted By IdahoPCCinc: 2 or 3 flute is GTG. A few things to remember with using either is correct rpm's for cutter diameter, width/depth of cut (face and Z) and direction of cut. Always be aware of how much stick out you have with your tooling. All this can be found with a little internet digging or getting a copy of the machinist's hand book, (look for a cheap used one) and it does help when it comes to preventing chatter, tool life, breaking shit, etc. Lubricant type can help with finish and cut quality too. . Originally Posted By IdahoPCCinc: Originally Posted By OneMoreAR: I always used a 2-flute endmill in aluminum. They can make big chips in the soft metal and allow clearance for those chips. 2 or 3 flute is GTG. A few things to remember with using either is correct rpm's for cutter diameter, width/depth of cut (face and Z) and direction of cut. Always be aware of how much stick out you have with your tooling. All this can be found with a little internet digging or getting a copy of the machinist's hand book, (look for a cheap used one) and it does help when it comes to preventing chatter, tool life, breaking shit, etc. Lubricant type can help with finish and cut quality too. . Also be aware of any coatings on the cutter. Don't use an end mill with AL in the coating, TiAlN for example, when cutting aluminum. The chips will weld to the cutter clogging the flutes. A well lubricated uncoated cutter works okay in aluminum but a simple TiN or TiCN coating is better. The coatings with AL in them are intended for ferrous metals only, at heat the AL converts to aluminum oxide giving a much harder, more wear resistant edge. |
Life's battles don't always go to the stronger or faster man. In the end, the one who wins is the one who thinks he can! - SCI, NRA
Team Ranstad
Team Ranstad
|
Originally Posted By TinSpinner:Also be aware of any coatings on the cutter. Don't use an end mill with AL in the coating, TiAlN for example, when cutting aluminum. The chips will weld to the cutter clogging the flutes. A well lubricated uncoated cutter works okay in aluminum but a simple TiN or TiCN coating is better. The coatings with AL in them are intended for ferrous metals only, at heat the AL converts to aluminum oxide giving a much harder, more wear resistant edge. I'll definitely keep an eye out for that in future shopping. |
Disclaimer - OP is bad at knowing things, and might catch on fire.
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman
Vet - Op MMAMA
Every other species kills off their stupid......we cater to them. -- spin-drift
Nobody ever called 911&said I just did something smart. -- TheFlynDutchman

| There's still one of these DRO's available from PM. I'm very happy with mine. |
